How to Read this Blog

When I started this blog, I could not figure out, within the given parameters, how to get it to read logically. So it ended up with the freshest post on the top of the page with the top of the post being the beginning of the post. When you get to the end of the post, you will find the beginning of the previous post. A bit awkward, but ...it is what it is. (right David?)

Also, feel free to leave comments. I engaged the annoying "real person verification thingy" because some dork put an add to his product on my blog and disguised it as a comment. He probably works on wall street.

Thursday, January 6, 2011

Clutch Master Cylinder to Clutch Pedal

Originally, this cab had a mechanical clutch, but the NV4500 has a hydraulic clutch. In the last post, I showed the work involved on the engine side of the firewall to convert this. Here is the interior side. You can see the master cylinder and rod coming through the firewall.
Here is the end of the rod in relation to the clutch pedal. I will need to fab up a bracket to reach from the pedal arm to the eye on the cylinder rod.
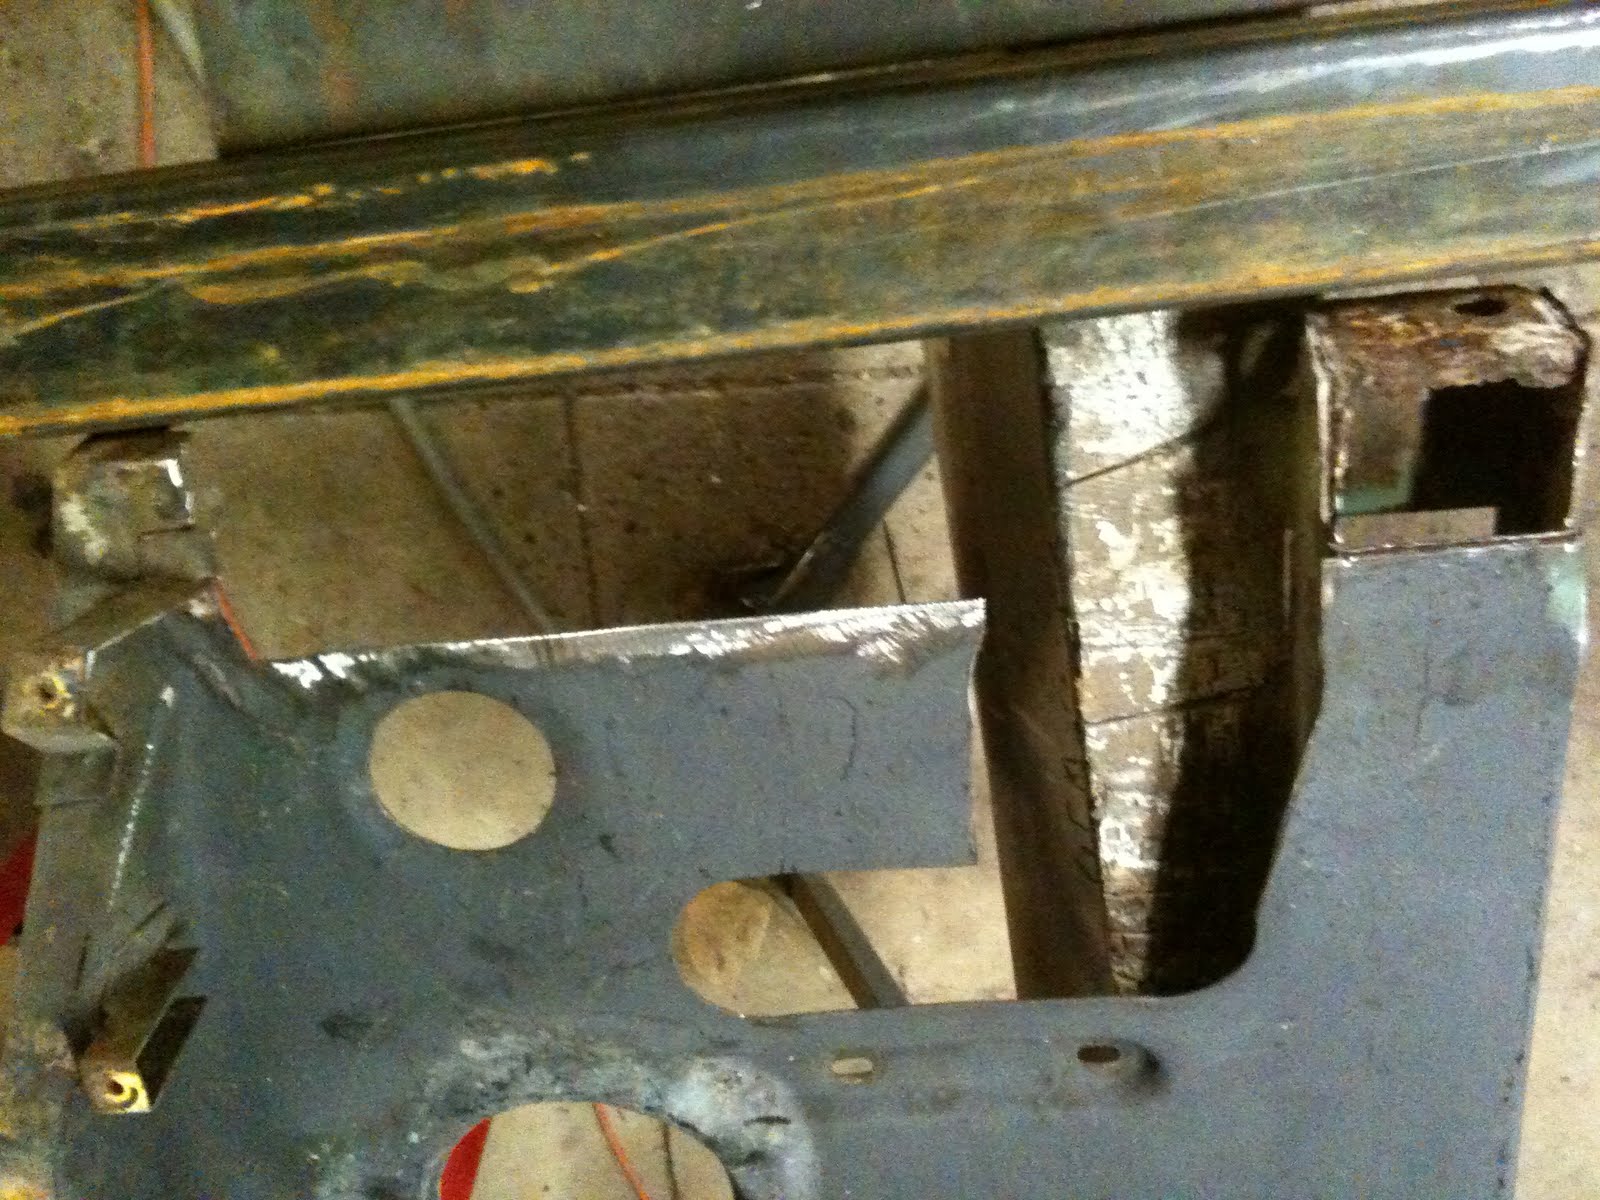
I started with this bracket. It is a piece that was bolted under the floor to support some of the mechanical clutch linkage. The tab on the left is about the width I need and the angle of the bend seems pretty close to what I need as well.
After some creative hacking with my port-a-band and some hammer and vice work, this is what I came up with. The long end with the hole in it will weld to the clutch pedal arm, and the end with my fingers will receive a hole for the pin that will go through the eye in the master cylinder actuator rod.
I noticed that the eye in the rod was hogged out a bit and did not want this to continue if I used a hardened bolt for a pivot pin so I thought about making some sort of bushing. Rummaging around in my brass drawer, I came up with this fitting. I figured I could use it to make a bushing.
I started by drilling out the center with a bit the same size as my bolt. I am thinking it was 1/2 inch, but it may have been 7/16 inch.
Nice fit so far.
Then, since I do not have a lathe, I chucked the bolt into my drill press. I used a nut on the bolt to keep the brass from spinning on the bolt. Then I used a file and sandpaper to "turn" the brass down...
...to the right size to fit the eye of the clutch rod. Then, I trimmed it to length to be just wider than the thickness of the eye.
Here the new bracket is clamped to the pedal with a vice grip. I welded a bolt in a hole in the bracket to act as a pin through the rod with the bushing. Then, I double-stacked the nuts to lock it in place while still allowing it to pivot.
And finally, after removing the pedal, I welded the bracket to the pedal. Job done.

More Firewall Thinking - Clutch Cylinder.

Back on December 20, Firewall Thinking, I sketched out what I thought would need to happen to get the clutch master cylinder in place.

Recycling this picture, it shows how the rectangle hole for the wiring harness bulkhead connector goes through. The circle shows the size and location of the hole needed for the clutch master cylinder (or so I thought).
I started by cutting a rectangle out of the driver's side of the hole.
Then, recycling the scrap rectangle, I planned to weld it on the other side of the hole. I used a magnet to hold the little piece in place as well as a hack saw blade that I used as a straight edge to ensure that the piece was in the right place.
After first tacking it in place, I burnt it in solid.
After grinding the welds smooth, I used a 2 1/2" hole saw to bore a hole to match the hole that was in the pattern I used that was a chunk of firewall from a 1st gen truck. I had to run into town to purchase the hole saw which makes the situation shown in the next pic all the more frustrating.
So, here I am welding a patch into this beautiful hole I just got through making.
It turns out that I really did not understand exactly how the master cylinder mounted in the hole and I am embarrassed to say I never compared the size of the barrel on the cylinder with the size of the hole in the pattern I used. It ends up that I am using a 2nd gen clutch hydraulic system (I think). It makes sense because I am using a 2nd gen transmission with the NV4500.
So, I had to resize the hole quite a bit smaller.
I cut some notches at 4 locations around the hole to fit ears that are on the cylinder. I forgot to take a pic of this, but I will edit one in later. The cylinder goes in from the engin side and twists 45 degrees to lock it in place. I also doubled the thickness of the firewall at this location to gice it a little more strength and support. The master cylinder reservoir will bolt to the cowl near where I am holding it.

Final Stages of Intercooler Mount

Since the new construction on the core support fit without issues, other than the mods I will need to make to the inner fenders to clear the inlet/outlet tubes, I went ahead and burned the rectangular tube to the the bottom of the core.
Next, I needed some brackets to support the isolators at the bottom of the intercooler. I made these by cutting a section of the same rectangular tube off the scrap end about 2 inches long. Then I drilled a 1" hole in each side of the section. Finally, I cut the section of tube on the diagonal to make two brackets like the one pictured below. The 1" hole receives the rubber button isolator that slides on a stud on the bottom of the intercooler.
This pictures the other side with the isolator in place. This locates and securely holds the bottom of the intercooler in the same way it was held in a factory application.
Next, I fabbed-up some upper mounts. This is a piece of 1" square tube with a 7/16 nut welded in the end. I am holding it with a pair of funky laminated vice grips. The right end is notched to fit flush with an indentation in the core support where the battery tray mounts.
Here it is welded in place with a slotted donut shaped isolator. I did the same on the other side. This located the top of the intercooler and keeps it from jumping out of the lower mounts.
Here is the core with the finished mounts and the intercooler (and ac condenser for that matter) securely mounted in place.
This is the engine side view showing the ac condenser and the in/outlets of the intercooler. Next will be supports for the radiator.

Working My Core

Before welding the 1.5 x 3 tube on the bottom of the core support, I wanted to make sure it would all fit together. I clamped the tube to the bottom and set the core in place. Then I hung one fender and propped the inner fender in place.
I needed to make sure there was ample room for the fender near the marker lamp. I had cut my tubing to be the same length as the width of the core support. The metal I cut away was not as bulky and tapered at the ends. With the tube cut off square, I could get my fingers between the end of the tube and the fender, so all is well here.
Then I set, or should I say, I tried to set the intercooler in place. I only did the test fit on the turbo side, but my problem became pretty obvious. The 1st gen intercooler inlet and outlet tubes are centered up and down on the intercooler. The 2nd gen cooler has inlet and outlet tubes on the bottom. The inlet tube shown hits the inner fender.
After studying this issue, it looks like I can massage the inner fender around the pipe. I do not think this will get the inner fender too close to the tire. In fact, I really can't see why the inner fender has this lump in it anyway. So, massaging the inner fenders gets added to my to-do list. I assume the left inner fender wil have the same issue.
Here is sorta how it looks with the intercooler almost in place.

Thursday, December 23, 2010

Today I cut the cheese.

er...I cut the rusty Swiss cheese metal out of the core.
Tacked in some new steel.
Burnt it in. Did the same on both sides.
Made some patches for the attachment sites.
Burnt them in as well.
This one looks better.

Wednesday, December 22, 2010

Today was a great day for grille-n.


I started this truck two years ago. From the beginning, I intended to keep the 1975/76 grille, ut I also wanted to have an intercooler. To make things worse, I planned to use a 2nd generation cummins intercooler, which is much bigger than the 1st generation intercooler. On top of all this, I will have air conditioning and will need a condenser behind the grille as well. This adds a lot of junk that was never intended to fit behind there. Well, today, with Hondo to keep me company, I figured it out.
Here is my original, rusty ol' core support. The long, oval-shaped holes are leftover from the 440 days. I used to get so much radiant heat in the cab that we would sometimes leave for camping in the middle of the night in the summer. I cut those holes to increase the air flow under the hood.
The first thing to go was this center grille support.
This is the 2nd gen intercooler. You can see The Great Vittorio in the background.
I forgot to tale some pictures, apparently. Maybe I will edit them in later. The next thing I hacked out of the core was a section of the box at the bottom so I could drop the intercooler as low as possible. This would take out some serious structure from this part that supports the hood, fenders, radiator, battery, etc, but I will combat that by grafting a piece of 1.5 inch box tubing along the bottom. By doing this, I will not need to use the body lift spacers under the core and it will be every bit as strong as original.

Then I had to cut a piece of the brace under the hood latch.

I am missing another picture here. Imaging how good the inter cooler looks with the top just under the above cut and the bottom flush with the bottom of the core support. I also blew some holes for the inlet and outlet tubes.

This shot shows the cooler under the grille. Now imagine the big ol' grin on my face. My teeth may even be showing.
The next thing to tackle is the condenser. On a 1st gen Dodge Cummins truck, the condenser is on the outside of the intercooler. There is now way this would fit behind this old school grille. My solution is to put the condenser between the radiator and the intercooler. I am hoping this will work. I do not know how much the intercooler will preheat the air before it reaches the condenser, but I will give it a try. To do this, the center support down the middle of the core support needed to go. In the picture below, you can see that I also cut out some of the metal below the condenser. I actually did not need to do this. I only needed to square the lower corners where they were rounded like the upper corners or the hole, as you can see in the pic. Since this core was all swiss-cheesey with rust that needs to be patched anyway, I just hacked it out of the way for now with a sawzall.This shot shows the missing center support. In the upper left corner, you can see where I marked for the hole for the connection point for the air conditioning hoses.So, now I have the condenser in, the intercooler in, the grille on, and the lower valance in place, well, almost.I'll try ti set this picture up. The silver on the right is the bottom lip of the grille. The little smile at the very top of the pic is the right turn signal lens hole. And, the long hole in the middle is the original hole in the 1975/76 valance. In the hole you can see the edge of the cooler. This is the part that is holding the valance out. The black lines are showing my plans for more chopping. In the pic, you can't see the contour of the metal, but if I cut this out, the valance will drop back at least an inch.
Rather than just chopping out what needs to come I will open up the whole hole. I hope to be able to make it look like it came this way. We'll see.
Here it is, engine side with the radiator in place.
Here, with the radiator out, you can see the connection block for the condenser.
This shot is looking down the hood latch opening. Red arrow = intercooler. Blue arrow = condenser. Yellow arrow = Radiator.
And, here it is all dressed for the party. I was so excited I even got out the ladder so I could get far enough away to get the hole thing in the picture.